Key Takeaways
Test your own printed files and production materials, not only a supplier’s prepared demonstration roll.
Agree on written pass/fail criteria for registration, cut depth, liner condition, waste removal and finished output.
Measure the complete job from file loading to accepted rolls or sheets; headline cutting speed is not usable throughput.
Include the smallest, longest and most complex regular jobs plus a difficult material and a repeat changeover.
Record the exact model, options, software and settings used so the demonstration matches the quotation.
The best way to test a digital label cutter before buying is to run a controlled factory acceptance test with your files, materials and finished-output specification. Measure registration across the job, inspect kiss and through cuts, time setup and production, challenge matrix removal, and verify slitting, rewinding or sheeting where required. Keep the samples and a signed configuration report.
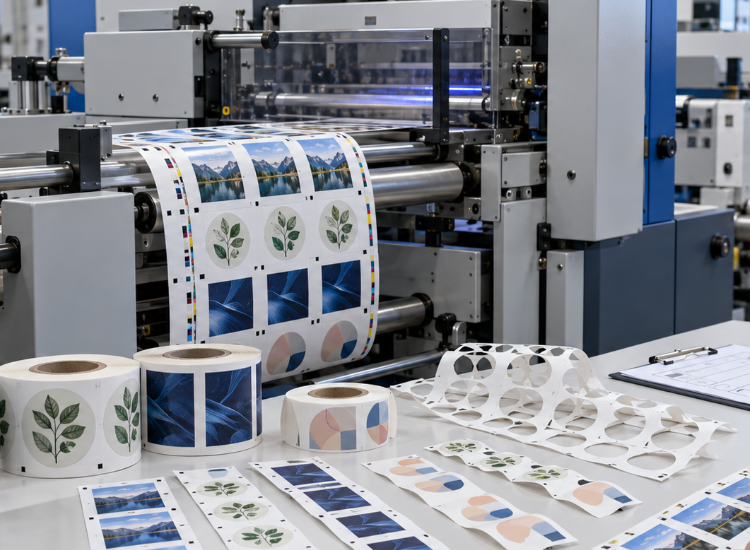
Step 1: Define the Jobs Before the Test
Choose three jobs that represent real production rather than three easy shapes.
| Test job | What it should reveal |
|---|
| Repeated simple label | Stable feeding and routine throughput |
| Small or detailed contour | Head movement, corners and usable speed |
| Long or multi-SKU job | Tracking, registration and job handling |
| Difficult regular material | Real compatibility and waste behavior |
Send the artwork, print file and cut file together. State whether each path is kiss cut, through cut, perforated or otherwise processed. Include actual roll width and diameter, facestock, adhesive, liner, lamination and finished format.
Step 2: Freeze the Quoted Configuration
Write down the model, number of cutting heads, sensor or camera, software version, web guide, lamination unit, matrix system, slitters, rewind shafts and optional sheeter. A successful test on a more highly configured machine does not prove that the quoted base configuration will reproduce it.
Ask who supplies the computer, air source, extraction, blades, holders, cores and software licenses. Note which functions are standard, optional or performed on separate equipment. VICUT’s roll label cutting range contains different architectures, so evaluation must remain model-specific.
Step 3: Set Written Acceptance Criteria
Avoid “looks good” as a result. Define what will be measured and how many samples will be checked.
| Area | Example acceptance question |
|---|
| Registration | Is the contour acceptable at the first, middle and final repeats? |
| Kiss cut | Does the label peel cleanly while the liner remains functional? |
| Full cut | Are edges clean and pieces controlled after separation? |
| Matrix removal | Does waste strip continuously at the agreed test condition? |
| Slitting | Do lane widths and edges meet the finished-roll specification? |
| Rewinding | Are cores, wind direction and roll build correct? |
| Changeover | Can the next saved job be loaded and approved predictably? |
Use tolerances from your product requirement and downstream equipment, not an invented universal figure.
Step 4: Test Print-to-Cut Registration
Place small circles, thin borders and shapes near different web positions. Inspect more than the centered sample. A uniform offset suggests an origin or sensor-to-tool issue; an error that grows along the roll may indicate print scale, web tracking or panel-reference problems.
Deliberately include the normal ink or toner, laminate and difficult surface. Observe how the machine responds to a missed mark: stop, retry, skip or continue. The operator should demonstrate the documented recovery procedure rather than manually rescuing every repeat.
Step 5: Verify Cut Quality and Liner Condition
Peel labels from several positions and inspect the release liner under controlled light. A top surface can appear clean while the liner is scored deeply enough to break during application. For through cuts, check corners, small internal features, retention method and output handling.
Run a fresh blade baseline and then document the tested blade type, exposure, pressure or force and number of passes. Settings belong to the full construction, not merely “paper” or “PET.”
Step 6: Challenge the Complete Finishing Path
If the quotation includes lamination, matrix removal, slitting and rewinding, test them together. Matrix stripping often exposes geometry or cut-depth problems that a stationary sample does not show. Finished rolls should be checked for lane width, edge alignment, winding direction, core fit and telescoping.
The VICUT VR320 label die cutter is documented with integrated finishing stations, whereas the VR30 roll label cutter has a different workflow. Confirm the quoted machine rather than transferring a feature between them.
Step 7: Measure Real Throughput
Start the timer when the operator opens or selects the job, not after the machine is already cutting. Stop when the output passes inspection and is ready for the next step. Record:
file preparation and job retrieval;
loading, threading and calibration;
mark reading and cutting;
matrix removal, slitting and rewinding;
stops, interventions and rejected material;
cleanup and changeover to the next job.
Calculate accepted labels per elapsed hour as well as meters processed. A small intricate label can produce a different result from a large simple contour even at the same web speed.
Step 8: Test Changeover and Recovery
Switch from one material and file to another, then recall the first job. Ask a normal operator—not only the supplier’s specialist—to perform the documented steps. Include a controlled stop, a missed mark and a material splice if these occur in normal production.
The goal is not to force a failure. It is to see whether the system reports the problem clearly, protects work already completed and returns to an approved state without hidden adjustment.
What to Keep After the Demonstration
Retain numbered input and output samples, photographs, measured results, job files, settings, test duration, waste quantity and the exact configuration list. Add any exceptions to the quotation. If a pass depends on a different sensor, extra heads or optional slitting unit, that difference must be visible before the purchase order.
VICUT’s guide to choosing a roll label die cutting machine manufacturer covers supplier evaluation. For the machine test itself, send VICUT the real job package and request a written report against your acceptance criteria.
Frequently Asked Questions
How many materials should I test?
Test the main production construction, the most difficult regular construction and one credible future material. More samples are useful only when each has a defined purpose.
Should I accept a video demonstration?
A video can screen a machine, but it does not replace traceable files, materials, measurements and configuration details for final acceptance.
Is maximum speed part of the acceptance test?
Yes, but only with the stated artwork, material and quality result. Also record total elapsed time and accepted output.
Who should approve the sample?
The person responsible for production quality and the downstream user or applicator requirement should approve it, not purchasing alone.
Arrange a Documented Sample Test With VICUT
Prepare the job files, printed rolls, material data and written pass/fail criteria before booking the demonstration. VICUT can then test a relevant digital roll label cutter against the required registration, cut depth, finishing functions and output format. Contact VICUT with the test package and ask for the exact model, options, settings and measured results to be recorded with the samples.
 vicutcnc@cncvicut.com